Product Description
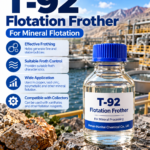
T-92 Frother is a flotation frother used in mineral processing to generate and maintain suitable froth during the separation of valuable minerals from gangue.
It is designed to provide effective bubble formation and controlled froth characteristics in flotation circuits. T-92 Frother can be used in selected copper, lead-zinc, polymetallic and other mineral flotation applications, depending on ore characteristics and the overall reagent system.
In practical flotation operations, frother performance should be evaluated together with the collector, pulp conditions, flotation equipment and required concentrate characteristics.
Hanhai Chemical supplies T-92 Frother for mining and mineral processing applications. Product specifications can be selected according to customer requirements, and COA and SDS are available upon request.
Product Specifications
| Item | Specification |
|---|---|
| Product Name | T-92 Frother |
| Product Type | Flotation Frother |
| Appearance | Liquid |
| Application | Mineral Flotation |
| Suitable Ores | Sulfide & Selected Mineral Ores |
| Grade | Mining / Industrial Grade |
| Origin | China |
Technical parameters may vary according to the supplied T-92 grade and manufacturing specification. Please refer to the latest COA for detailed physical and chemical properties.
Applications
Copper Ore Flotation
T-92 Frother can be used in selected copper ore flotation circuits to help generate suitable bubbles and maintain the froth layer required for mineral recovery.
It can be combined with appropriate collectors according to ore mineralogy and flotation conditions.
Lead-Zinc Ore Flotation
In selected lead and zinc sulfide ore flotation systems, T-92 can be used to provide the frothing conditions required for mineral separation.
The final dosage and reagent combination should be optimized according to the specific ore and flotation process.
Polymetallic Ore Flotation
T-92 Frother can also be considered for complex polymetallic ore flotation, where several valuable minerals need to be separated or recovered.
Froth characteristics should be matched with the collector system and separation sequence.
Other Mineral Flotation
T-92 may be evaluated for other mineral beneficiation processes where controlled bubble generation and suitable froth stability are required.
Laboratory flotation tests are recommended when introducing the frother into a new ore or reagent system.
How T-92 Works in Flotation
In froth flotation, different reagents perform different functions.
Collectors help increase the hydrophobicity of selected mineral surfaces, while T-92 Frother helps create and maintain the bubble and froth environment needed for flotation.
Depending on the flotation system, T-92 can help:
- Promote suitable bubble formation
- Maintain controlled froth characteristics
- Support mineral-loaded bubbles entering the froth layer
- Improve flotation operating stability
- Work together with commonly used flotation collectors
Frother performance depends strongly on ore mineralogy, particle size, pulp pH, water chemistry, collector system and flotation equipment.
Product Advantages
Effective Frothing Performance
Provides the frothing action required for selected mineral flotation processes.
Suitable Froth Control
Helps maintain suitable bubble and froth characteristics during flotation.
Wide Mineral Application
Can be evaluated for copper, lead-zinc, polymetallic and other mineral flotation systems.
Compatible with Common Collectors
Can be used in suitable reagent systems containing xanthates, dithiophosphates and other flotation collectors.
Application-Based Reagent Selection
T-92 selection and dosage can be discussed according to the customer’s ore type, target mineral and existing flotation reagent system.
Stable Export Supply
COA, SDS, export documentation and suitable packaging can be provided according to order requirements.
T-92 Frother vs. MIBC and Pine Oil
Different frothers can produce different bubble and froth characteristics.
MIBC is commonly selected where relatively controlled froth characteristics are required.
Pine Oil is another widely used frother in mineral processing and can provide effective frothing under suitable operating conditions.
T-92 Frother provides another option for flotation plants and should be evaluated according to the actual ore and reagent system.
There is no single frother that is optimal for every ore. Laboratory or plant testing is recommended when changing frother type.
Packaging & Storage
T-92 Frother is supplied in suitable industrial liquid packaging according to product specification, transportation requirements and customer needs.
Available packaging should be confirmed before ordering.
Store in a cool, dry and well-ventilated area with containers tightly closed.
Keep away from heat and other incompatible conditions specified in the product SDS.
Handling, storage and transportation should follow the latest SDS and applicable regulations.
Why Choose Hanhai Chemical
Hanhai Chemical supplies flotation reagents and related chemicals for mineral processing applications.
Our flotation reagent range includes:
- T-92 Frother
- MIBC
- Pine Oil
- Xanthate Collectors
- Dithiophosphate Collectors
- Flocculants
- Mineral Processing Water Treatment Chemicals
Instead of selecting a frother only by product name, customers can provide their ore type, target mineral, current collector, current frother, reagent dosage and flotation problem.
This information helps us discuss a more suitable flotation reagent and supply solution for the actual mineral processing application.
FAQ
What is T-92 Frother used for?
T-92 is used as a frother in mineral flotation. Its main role is to help create and maintain suitable bubbles and froth during the flotation process.
Is T-92 a collector?
No. T-92 is primarily used as a flotation frother.
Collectors and frothers perform different functions in a flotation reagent system.
Which ores can T-92 Frother be used for?
T-92 can be evaluated for selected copper, lead-zinc, polymetallic and other mineral flotation applications. Actual suitability depends on the ore and flotation conditions.
Can T-92 be used with xanthates?
T-92 can be used in suitable flotation systems together with xanthate collectors and other flotation reagents.
The reagent combination should be optimized according to the specific ore.
Is T-92 the same as MIBC?
No. T-92 and MIBC are different flotation frother products.
Their performance and suitable operating conditions may differ, so selection should be based on the actual flotation process rather than treating them as identical products.
How do I determine the T-92 dosage?
There is no universal dosage suitable for every flotation plant.
The dosage should be optimized according to ore characteristics, flotation equipment, collector system, pulp conditions and required froth characteristics.
Can you provide COA and SDS?
Yes. COA and SDS can be provided for the supplied T-92 Frother specification.
Inquiry
Looking for T-92 Frother for mineral flotation?
Contact Henan Hanhai Chemical Co., Ltd. and provide:
Ore Type + Target Mineral + Current Collector + Current Frother + Dosage + Flotation Problem + Required Quantity + Destination
We can discuss the appropriate T-92 specification, packaging, quotation and export supply solution according to your flotation process.