Integrated Chemical Manufacturing & Supply for Global Industries
About Us
Reliable Chemical Manufacturing & Supply Since 2008
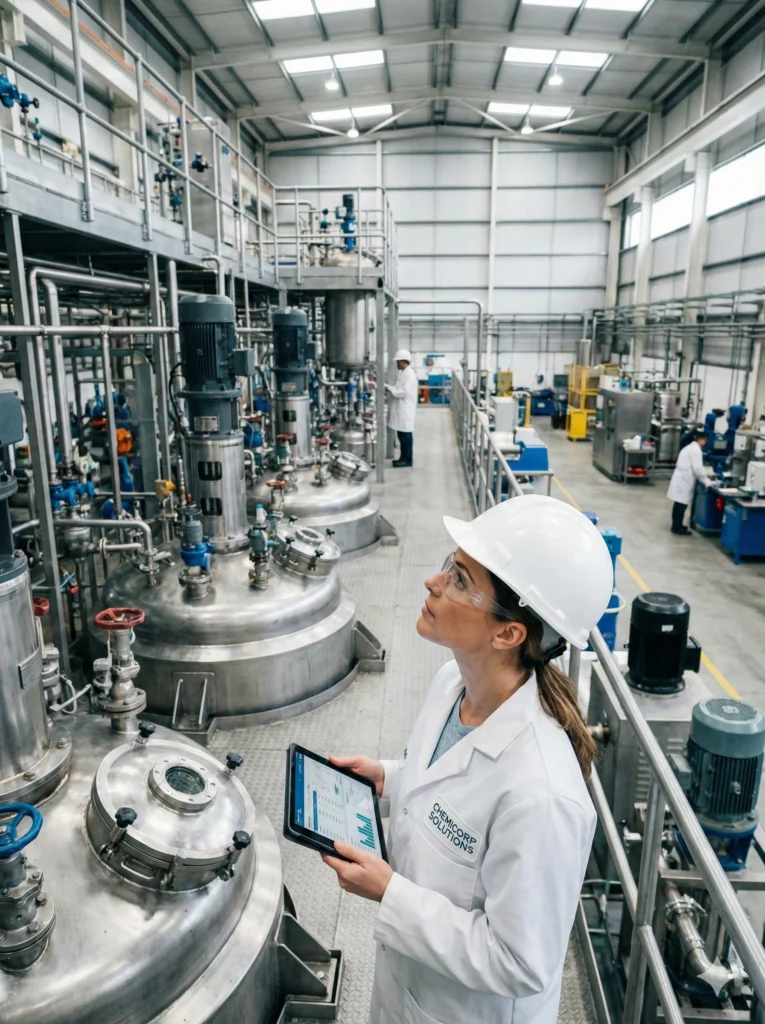
Founded in 2008, Henan Hanhai Chemical Co., Ltd. is an integrated chemical enterprise combining manufacturing, quality control and international supply services. We focus on industrial chemicals for mining, water treatment and oilfield applications.
Our product portfolio covers flotation reagents, collectors, frothers and mineral processing chemicals; PAM, PAC and specialty water treatment polymers; as well as chemicals for drilling, fluid treatment and other oilfield operations. Multiple grades, specifications and packaging options are available for different industrial requirements.
With manufacturing capabilities and established production resources, Hanhai Chemical provides customers with consistent quality, flexible supply and professional export support—from product selection and documentation to packaging, logistics and delivery.
Specialized Chemicals for Critical Industrial Applications
Hanhai Chemical focuses on chemical supply for mining, water treatment and oilfield applications. Our product portfolio covers mineral processing reagents, water treatment polymers and oilfield chemicals, with flexible specifications and supply solutions for different operating conditions.
Mining & Flotation Chemicals
Flotation reagents, collectors, frothers, sodium sulfide and other chemicals for mineral processing applications.
Water Treatment Polymers
PAM, PAC and specialty polymers for solid-liquid separation, clarification and industrial wastewater treatment.
Oilfield Chemical Solutions
Chemicals for drilling, fluid treatment and oilfield operations, with specifications available for different application requirements.
Flexible Specifications & Supply
Multiple grades, specifications and packaging options to meet different industrial and regional requirements.
Reliable Chemicals for Mining, Water Treatment & Oilfield
Manufacturing Capability · Flexible Supply · Professional Export Service